Stone Wool Insulation
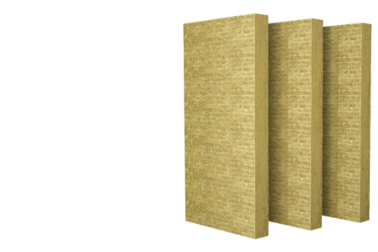
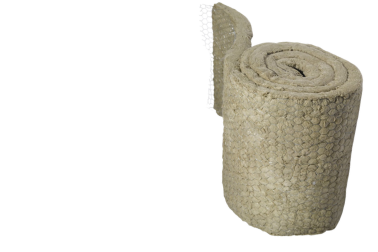
We supply high-performance stone wool insulation products, a type of mineral wool made from volcanic rock. Our range includes Rockfibre Boards and Wired Mats, designed to deliver excellent fire resistance, acoustic performance, and thermal efficiency for both new construction and renovation projects across residential, commercial, and industrial sectors throughout South Africa.
Why Choose Stone wool?
Superior Fire Protection
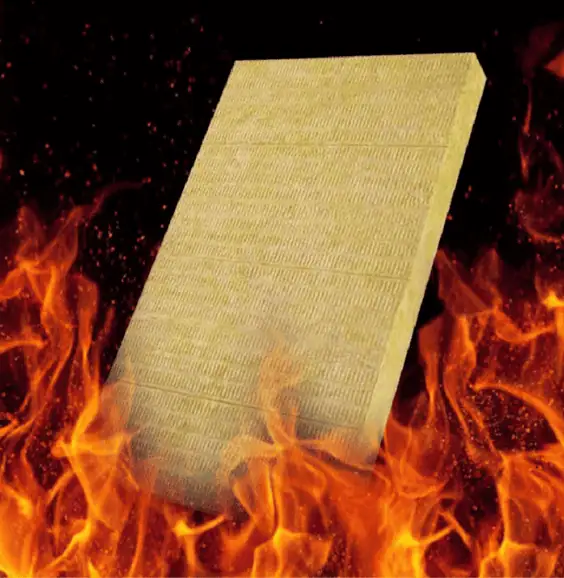
Stone wool provides superior fire resistance, making it ideal for commercial buildings, offices, and public spaces where safety regulations are strict. It’s natural mineral composition allows them to withstand extremely high temperatures without releasing toxic smoke or losing structural integrity.
Key Benefits:
- A1 non-combustible rating – highest fire safety classification
- Maintains structural integrity at temperatures up to 750°C
- Excellent for fire-rated walls, ceilings, and compartmentation
- Does not contribute to fire spread or smoke development
- Compliant with South African National Building Regulations
- Long-term durability with no degradation over time
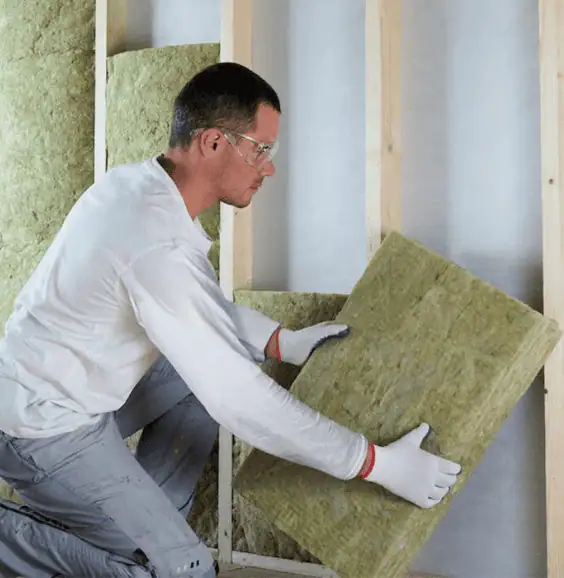
Acoustic Insulation
Stone wool is highly effective at absorbing sound, making it an excellent choice for acoustic insulation in offices, recording studios, homes, cinemas, and commercial buildings. Its dense fibrous structure disrupts sound waves, significantly reducing noise transmission between rooms and improving overall acoustic comfort.
Key Benefits:
- High sound absorption with excellent NRC values
- Effectively reduces airborne and impact noise
- Ideal for offices, meeting rooms, studios, and residential spaces
- Improves speech privacy and reduces echo
- Maintains acoustic performance over many years
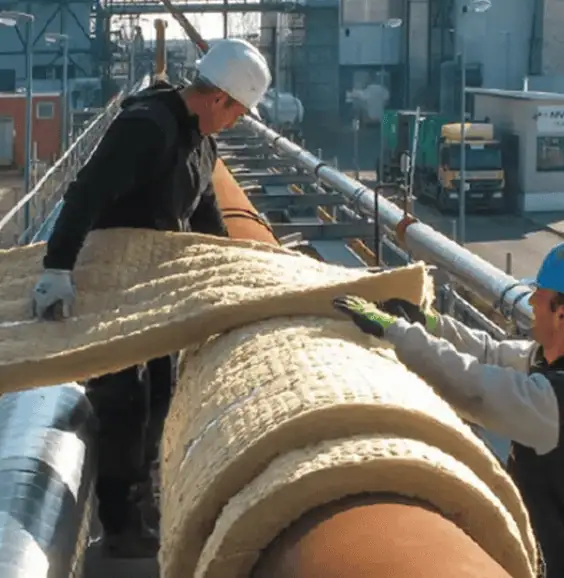
Industrial Insulation
Rockwool insulation is widely used across industrial sectors due to its excellent thermal performance, fire resistance, and durability in demanding environments. It is commonly applied in factories, power plants, refineries, and processing facilities where reliable insulation is critical for energy efficiency and safety.
Key Benefits:
- High thermal resistance for industrial processes
- Continuous high temperatures without degradation
- Non-combustible with A1 fire rating
- Resistant to vibration, moisture, and chemical exposure
- Suitable for boilers, furnaces, pipework, and plant rooms
- Long service life with minimal maintenance